-
What Actually Happens When a Linear Actuator Fails
-
Step 1: Find Out What Actually Failed
-
Step 2: Write Down the Exact Part Identification
-
Step 3: Check the Universal Joint Coupling First
-
Step 4: Compare Total Cost, Not Just the Unit Price
-
Step 5: Match the Series and Configuration, Not Just the Brand
-
Step 6: Buy From Someone Who Can Answer a Dumb Question
-
Step 7: Fix the Root Cause Before You Reinstall
-
Mistakes I Keep Seeing in the Cost Log
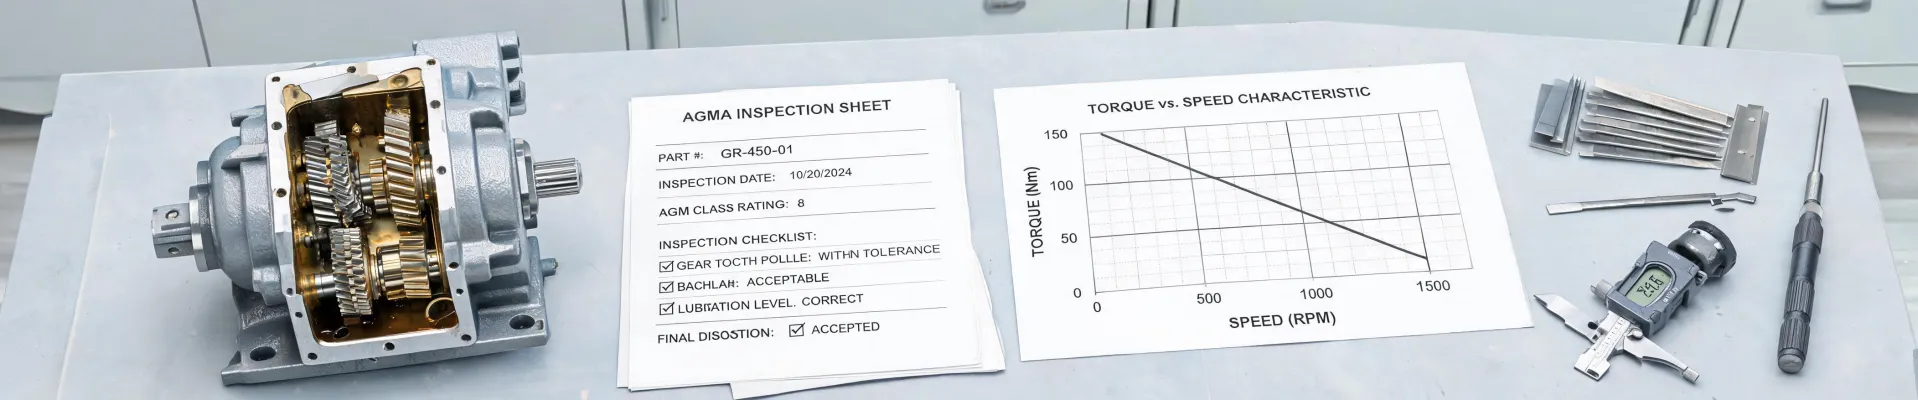
Quick clarification before the checklist: if you searched “boston sports gear” while shopping for uniforms or workout clothes, you’re in the wrong place. Boston Gear is an industrial motion control manufacturer, not a sporting goods store. They make speed reducers, gearboxes, motors, linear actuators, and couplings. If you have a machine down and you’re wondering what happens when a linear actuator fails, this page is for you.
I’m a procurement manager at a packaging company with about 300 employees. I’ve managed the repair-parts budget—roughly $380,000 a year—for six years, and I log every order in our cost tracking system. This is the checklist I use when a linear actuator stops.
What Actually Happens When a Linear Actuator Fails
It’s rarely a dramatic explosion. Most linear actuator failures start with warnings: the stroke takes a little longer, the motor drive logs an overcurrent event, or you hear a rough noise near the end of travel. In a plant that’s running, those warnings get ignored until the machine stops.
Once it stops, the damage compounds. A worn leadscrew nut or a binding carriage makes the linear actuator motor pull more current. The drive gets hot. If overload protection doesn’t catch it, the motor burns out. Meanwhile, the extra strain finds the weakest mechanical link—usually the universal joint coupling or the rod end bearing. By the time you open the machine, you often have several damaged parts, not one.
Step 1: Find Out What Actually Failed
An “actuator overload” alarm is a symptom. It is not a diagnosis. I learned that with a $680 mistake in 2023.
Our carton pusher kept tripping. The maintenance tech was sure the linear actuator motor was burned out, so I expedited a replacement. We installed it in under 24 hours, and it tripped again within an hour. The real problem was a cracked universal joint coupling that was binding under load. The coupling cost $54. The motor cost $680 plus overtime. Now we inspect the mechanical path before we order electrical parts.
Do this before you pick up the phone:
- Disconnect the motor from the actuator and turn the shaft by hand. Does it spin smoothly, or does it catch in spots?
- Move the actuator through its full stroke with no load attached. Listen for grinding and watch for jerky movement.
- Inspect the universal joint coupling, the rod end, and the mounting bolts for looseness, cracks, or wear.
Step 2: Write Down the Exact Part Identification
Once you know which part failed, get the full identification from the nameplate—not from memory, and not from last year’s spare parts list. The part sitting on the bench is the only source of truth.
This seems obvious until you do it wrong. I’ve seen a motor ordered by frame size without checking the winding voltage. I’ve seen an actuator ordered by stroke length without checking the rod end thread. It’s not the distributor’s fault. There isn’t enough information.
Take a clear photo of the nameplate. Photograph the mounting arrangement and the damaged part too. Send those photos to the supplier. It takes two minutes and prevents a whole category of return shipments.
Step 3: Check the Universal Joint Coupling First
The universal joint coupling is often the cheapest part in the assembly, which is exactly why it gets ignored. When an actuator is mounted with even a small misalignment, the universal joint coupling is the component that absorbs the error. It also sees the least lubrication and the most vibration.
A worn u-joint creates backlash. Backlash causes vibration. Vibration wears the leadscrew, the guide rails, and the rod end faster. Then the motor has to work harder to hold position. From the outside, the actuator looks fine, so a rushed buyer replaces the whole $900 actuator when the actual problem was a $45 coupling.
In our cost logs, about 30 percent of reported actuator failures over a two-year stretch had a bad coupling or rod-end bearing as the root cause. The actuator itself was still usable. Some of those units went back into service after we changed the linkage parts.
Step 4: Compare Total Cost, Not Just the Unit Price
The decision that lands on my desk is always the same: repair or replace, and if replace, buy from whom? I don’t compare sticker prices. I compare all-in cost over the expected life.
Here’s a real example. A burned-out linear actuator motor had to be replaced. An established supplier had the correct motor in stock for $412 with next-day delivery. An online listing had a similar motor for $239, but it wouldn’t ship for another week. On paper, the $239 motor looks better. It isn’t. Our line loses about $2,100 per hour when it’s down. A week of extra waiting isn’t $173 in savings. It’s five figures in lost throughput.
I’m not saying lower-priced parts are automatically dangerous. But that lower price has to be multiplied by downtime, freight, installation labor, any adapter plates or brackets, and the probability of a repeat failure. That calculation is what total cost means.
Step 5: Match the Series and Configuration, Not Just the Brand
Boston Gear’s catalog includes speed reducers, gearboxes, motors, bearings, and actuators. But “Boston Gear” alone is not a specification. There’s a reason people search for “boston gear 300 series” rather than just the brand name: the product family matters. A 300 series gearbox is not necessarily interchangeable with another gearbox family from the same manufacturer. Even inside one series, you still have to match the ratio, input flange, output shaft, and mounting position.
The same applies to a linear actuator. Everyone remembers the stroke length and the push force. The voltage, the duty cycle, the retracted length, and the rod end thread often get skipped. Those skipped details are what cause a replacement to arrive and not fit.
When the quote comes back, ask the supplier to confirm that each mechanical and electrical specification matches your old part. Get it in writing. A three-sentence email is cheap; a return label is not.
Step 6: Buy From Someone Who Can Answer a Dumb Question
I understand time pressure. I’ve had two hours to make a call before a weekend production run, and my normal process says “get three quotes.” That isn’t always possible. When the timeline collapses, I go with the supplier who can answer questions, not just process payment.
There’s a reason Boston Gear has a distributor network instead of selling only through anonymous listings. Motion applications are not all the same. A good distributor asks about load, duty cycle, ambient temperature, and mounting orientation. That five-minute conversation has saved me from buying the wrong actuator more than once.
One example: I called about a replacement actuator expecting a quick order. The engineer asked about the duty cycle. Our process was cycling well above the continuous rating of the actuator I was about to buy. He recommended a larger model with a different leadscrew, and that station hasn’t failed since. A listing on the internet would have just taken my money.
Step 7: Fix the Root Cause Before You Reinstall
The last step is the easiest to skip because it doesn’t involve a purchase order.
If a linear actuator motor burned out, something made it work too hard. It might be old age. But it might be a loose mount, a misaligned shaft, or a drive parameter that’s set wrong. Install a new actuator over the same root cause, and you’ve just scheduled the next failure.
Before reassembly, check the alignment between the motor and the gearbox, the alignment of the actuator with the load, the torque on the mounting bolts, and the condition of the flexible coupling. Verify the drive settings against the motor nameplate. Take a photo of the installation for the maintenance log. It costs about 30 minutes and usually doubles the life of the replacement.
Mistakes I Keep Seeing in the Cost Log
These three mistakes show up in our records no matter which brand or supplier we use:
- Replacing look-alikes. Two actuators can have the same stroke and the same frame but different force ratings, voltages, or IP ratings. If the machine runs in a washdown area, an IP54 unit won’t survive as long as the IP65 it replaced, even if the price was much lower.
- Only comparing the quote. The quote is not the cost. Once you add freight, installation, downtime, and the probability that an unbranded part doesn’t meet its datasheet, the cheapest line item can cost the most overall.
- Skipping the root-cause check. The most expensive replacement is the one you install twice. Log what failed, why it failed, and what changes you made before you put the machine back in service.
My experience is built on roughly 300 replacement orders in packaging and conveyor applications, and those numbers come from our own cost tracking, not from an industry study. If you work with heavy cranes, medical devices, or something outside that range, your specific numbers will differ. The sequence, though, should stay the same: diagnose first, match the exact part, calculate total cost, buy from someone technical, and fix the root cause before you reassemble.
Elena Markovic
Elena Markovic is an independent industrial motor and drive systems analyst covering induction motors, servo motors, stepper motors, and variable-frequency drives. She examines IEC 60034-30-1 efficiency classes, IEC 61800-9-2 drive-system losses, speed-torque curves, duty cycles, thermal limits, and feedback compatibility across operating envelopes. Her evidence-led guides help OEM engineers and plant teams select efficient motion packages, plan integration, and reduce commissioning risk.