-
Why I'm Confident Saying This
-
What Actually Breaks When an Actuator Fails
-
The TCO Math: How a $260 "Savings" Cost $9,600
-
Why Boston Gear Reducers Keep Showing Up in Emergencies
-
The Stepper Motor Controller: The Part Everyone Remembers Too Late
-
What About Linear Induction Motors?
-
When the "Replace Everything" Approach Is Wrong
-
Bottom Line
When a linear actuator fails, the actuator is the cheapest part of the problem.
Seriously. I've spent three years coordinating emergency motion control replacements, and the pattern is relentless: a positioning axis stalls, maintenance swaps the actuator, the line restarts. Then it fails again a week later. The replacement actuator "worked." The failure just wasn't contained to the actuator.
Here's the conclusion you need before the rest of this: a linear actuator failure is a system failure, not a component failure. Replace only the actuator, and you're betting that the reducer, the stepper motor controller, the coupling, and the cabling all survived the event. Based on repairs I've tracked across 200+ rush orders, that bet loses about a third of the time. And the second failure is always more expensive than the first.
Why? Because downtime dominates the cost. According to Aberdeen Group's 2024 research, unplanned downtime in manufacturing costs an average of $260,000 per hour. At a mid-size packaging plant, one hour of downtime can erase the profit on an entire week of production. The $500 actuator is a rounding error next to that.
Why I'm Confident Saying This
I'm a senior distribution coordinator at a motion control supply company. I've handled 200+ rush orders in three years, including same-day turnarounds for food processing, packaging, and automotive clients. When a plant goes down, I'm the person they call to find parts in hours instead of weeks.
One case sticks with me. In March 2024, a packaging client in Ohio called at 2:00 PM on a Thursday. Their labeling line was dead—failed linear actuator—and they had a retail customer deadline in 48 hours. Normal lead time on the replacement parts was five days.
We located a Boston Gear reducer and a compatible stepper motor controller at a regional distributor. The catch: we had about three hours to confirm the order before the distributor's Friday truck schedule closed. Normally I'd compare three vendors and sleep on it. There was no time. Went with the Boston Gear distributor on trust alone. Paid a $250 expedite fee on top of the $1,850 base cost, and had both components on-site by Saturday 10 AM. The line was running by noon. Missing that deadline would have triggered a penalty clause worth roughly $50,000. That $250 rush fee was the cheapest insurance we bought all quarter.
Not an unusual story, unfortunately. Last quarter we processed 18 rush orders with 95% on-time delivery. Every successful recovery had one thing in common: the client made decisions based on total cost, not unit price.
What Actually Breaks When an Actuator Fails
Most people picture a linear actuator as a simple push-pull device. It's not. An electromechanical linear actuator is a small stack of systems working together:
- The motor—typically a stepper or servo motor
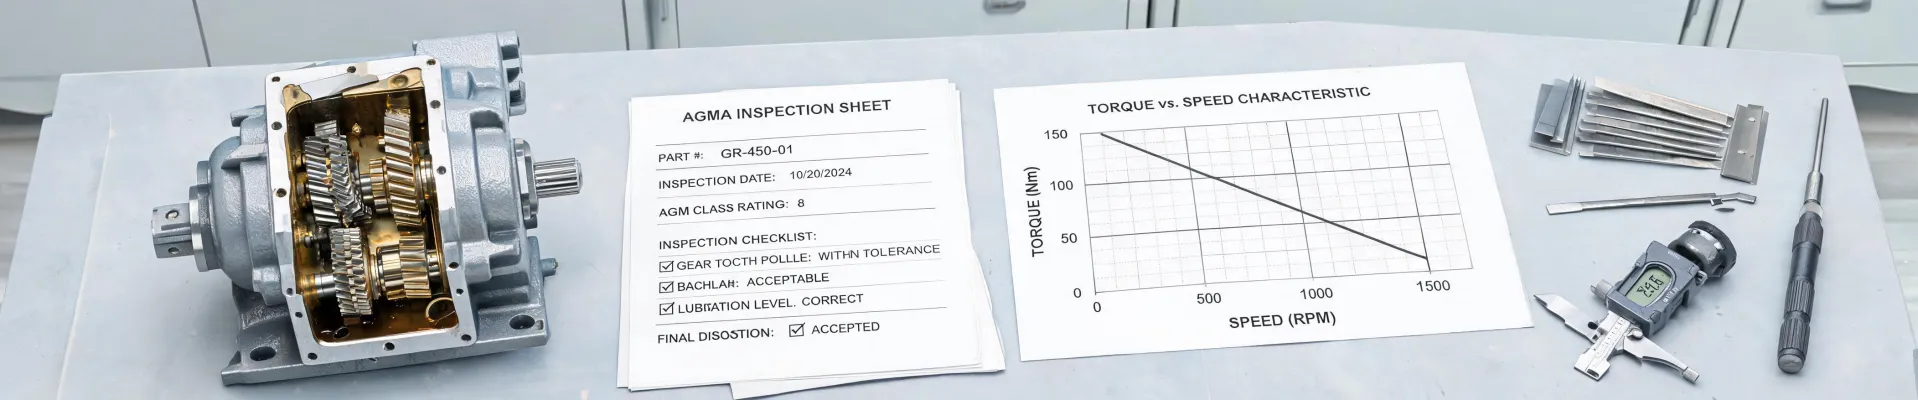
- A gear reducer, often a Boston Gear 700 Series unit on legacy equipment
- A screw mechanism (ball screw or lead screw) converting rotary motion to linear travel
- Guide rails or linear bearings
- A controller and driver electronics on the electrical side
When the actuator jams or overloads, damage can cascade through all of those. A sudden stall can back-drive the gearbox and chip gear teeth. An overloaded stepper motor can send voltage spikes into the controller and kill the driver. A misaligned coupling can destroy motor bearings. Not a single one of those failures is visible until the axis fails again.
That's why I push clients toward complete axis replacement in urgent situations. It feels wasteful. The reducer looks fine; the controller's LED is still glowing. But in a rush scenario, you don't have time for a second failure. And a second failure is exactly what happens when you fix the visible problem and ignore the hidden ones. Worse than expected, honestly.
The TCO Math: How a $260 "Savings" Cost $9,600
Here's a real comparison from a July 2024 order. A client needed a replacement linear actuator fast. Two options:
Option A: a $420 actuator from an online source. Expedited shipping from overseas: $140. Lead time: four to five days.
Option B: a $680 Boston Gear actuator stocked by a regional distributor. Next-day delivery at $60 freight. Application support included.
The price gap was $260. If you only look at unit price, Option A wins it. The client hesitated—a 62% premium is real money.
But that client's line was generating $4,800 per day in contribution margin. Option A meant four to five days of downtime—$19,000 to $24,000 in lost production. Option B meant two days—$9,600. The $260 difference vanished next to a $10,000 swing in downtime. We laid out that math side by side. The hesitation didn't last long.
That's the total cost of ownership framework. The unit price is the most visible number, but it's rarely the most important one. TCO includes freight, lead time, engineering support, risk of failure, and—in production environments—the hourly value of the line you're stopping. The question everyone asks is "what's your best price?" The question they should ask is "what's included in that price, and what does one extra day of delay cost me?"
Why Boston Gear Reducers Keep Showing Up in Emergencies
I'm not going to tell you the Boston Gear Company is the only reliable supplier for motion control. That would be a disservice to some good competitors. But the brand appears constantly in my emergency work, for practical reasons.
Documentation. Boston Gear has published full technical catalogs for decades. The 700 Series catalog is one of the most complete references in the industry for speed reducers, gears—spur, worm, bevel—and motion control components. When I need mounting dimensions, shaft sizes, or ratios under pressure, that documentation is gold.
Interchangeability. Older production lines are full of Boston Gear reducers. When a reducer is part of a failed axis, the fastest path to a running line is often the same product with the same known dimensions. No surprises.
Distributor depth. Boston Gear distribution is genuinely deep. That means stock on real shelves, humans who can answer compatibility questions, and next-day delivery in most industrial regions. In a crisis, that depth often decides whether you're down two days or five.
The Stepper Motor Controller: The Part Everyone Remembers Too Late
If the actuator is the visible victim, the stepper motor controller is the hidden one.
A stepper motor controller isn't just a switch box. It regulates current, manages microstepping, processes limit switch logic, and protects the motor. When a mechanical jam happens, the motor can back-feed voltage spikes or draw overcurrent. The controller might fail immediately, or it might be damaged and die three days later—after you've already restarted the line.
My rule, developed over all those rush orders: if an axis failed mechanically, bench-test the controller with the new actuator before declaring victory. It takes 20 minutes. It has saved our clients more second service calls than I can count.
What About Linear Induction Motors?
This question comes up more than you'd think. A linear induction motor (LIM) produces linear motion directly through electromagnetic force. No screw. No reducer. No rotating motor. For very high speed or long stroke applications—rail transit, high-throughput sortation, automated picking—a LIM can be an excellent design choice.
But here's the blunt part: a LIM is not a drop-in replacement for a screw-driven linear actuator. It needs different control electronics, different feedback, different mechanical mounting. Converting a working axis to a LIM is a redesign, not a part swap. In the middle of a production failure, you want the axis restored to its known-good configuration. A technology upgrade belongs on a planned timeline with a documented business case, not in a crisis.
When the "Replace Everything" Approach Is Wrong
I've spent this article arguing for speed and full-axis replacement. The honest limit: those rules don't apply everywhere.
Repeat failures are a system problem. If the same actuator fails more than once a year, stop replacing it. The root cause is probably undersizing, miscalculation, or a design flaw. A rush replacement is just rehearsal for the next failure.
Repair can beat replacement. On larger units, rebuilding the screw or replacing reducer bearings can restore performance at 30–40% of the cost of a new assembly. The catch is time—repairs take weeks, not days. Lousy emergency solution. Excellent planned one.
Check the input power. I've seen two consecutive controller failures traced to a sagging power supply in the control cabinet. First looked like an actuator problem. Second looked like another controller problem. Real cause was cabinet power all along. The basics will get you every time.
And about rush fees: as of January 2025, expedited freight typically adds 25–100% over standard rates, depending on carrier and distance. If you're paying premium freight on every failure, the problem isn't your supplier—it's your spares strategy. Every plant running production-critical linear actuators should have a complete axis kit (actuator, controller, coupling) on the shelf. I know that sounds like odd advice from someone who gets paid to solve emergencies. But honestly? I'd rather sell you one spare kit than three rush orders.
Bottom Line
So what happens when a linear actuator fails? If your answer is "we'll swap the actuator and restart," your line will probably go down twice. The better answer: calculate the hourly value of your downtime, inspect the whole axis, bench-test the controller, and then pick the option that gets the system verified and running in the fewest hours. That's TCO. That's the job.
Boston Gear reducers, matched stepper motor controllers, and a distributor who answers the phone—those are the tools that turned 17 of our 18 rush orders into successful recoveries last quarter. The brand isn't magic. The process is.
Prices and lead times change, so verify current rates before you commit (prices referenced as of January 2025). And if you're reading this before your next emergency: good. Build the spares plan now. The line will thank you later.
Elena Markovic
Elena Markovic is an independent industrial motor and drive systems analyst covering induction motors, servo motors, stepper motors, and variable-frequency drives. She examines IEC 60034-30-1 efficiency classes, IEC 61800-9-2 drive-system losses, speed-torque curves, duty cycles, thermal limits, and feedback compatibility across operating envelopes. Her evidence-led guides help OEM engineers and plant teams select efficient motion packages, plan integration, and reduce commissioning risk.